
Toolpath › Toolpath builds a milling path for one selected mesh; its tooltip reads "Build z-constant tool path for the given mesh". Use it to check how a part can be milled from the top: the result is a G-code object that you can play in G-code Visualizer or turn into a Swept Volume.
Orient the part along Z
The tool always comes from above: the path is built for the +Z direction, and Safe Z is a height above the top of the part. Before you build a path, turn the part so that the side to mill faces +Z. Use Transform › Align to Plane, 3-2-1 Align or the Rotation XYZ fields of the Transform block under the Scene tree. The path is built for the part as it is placed in the scene.
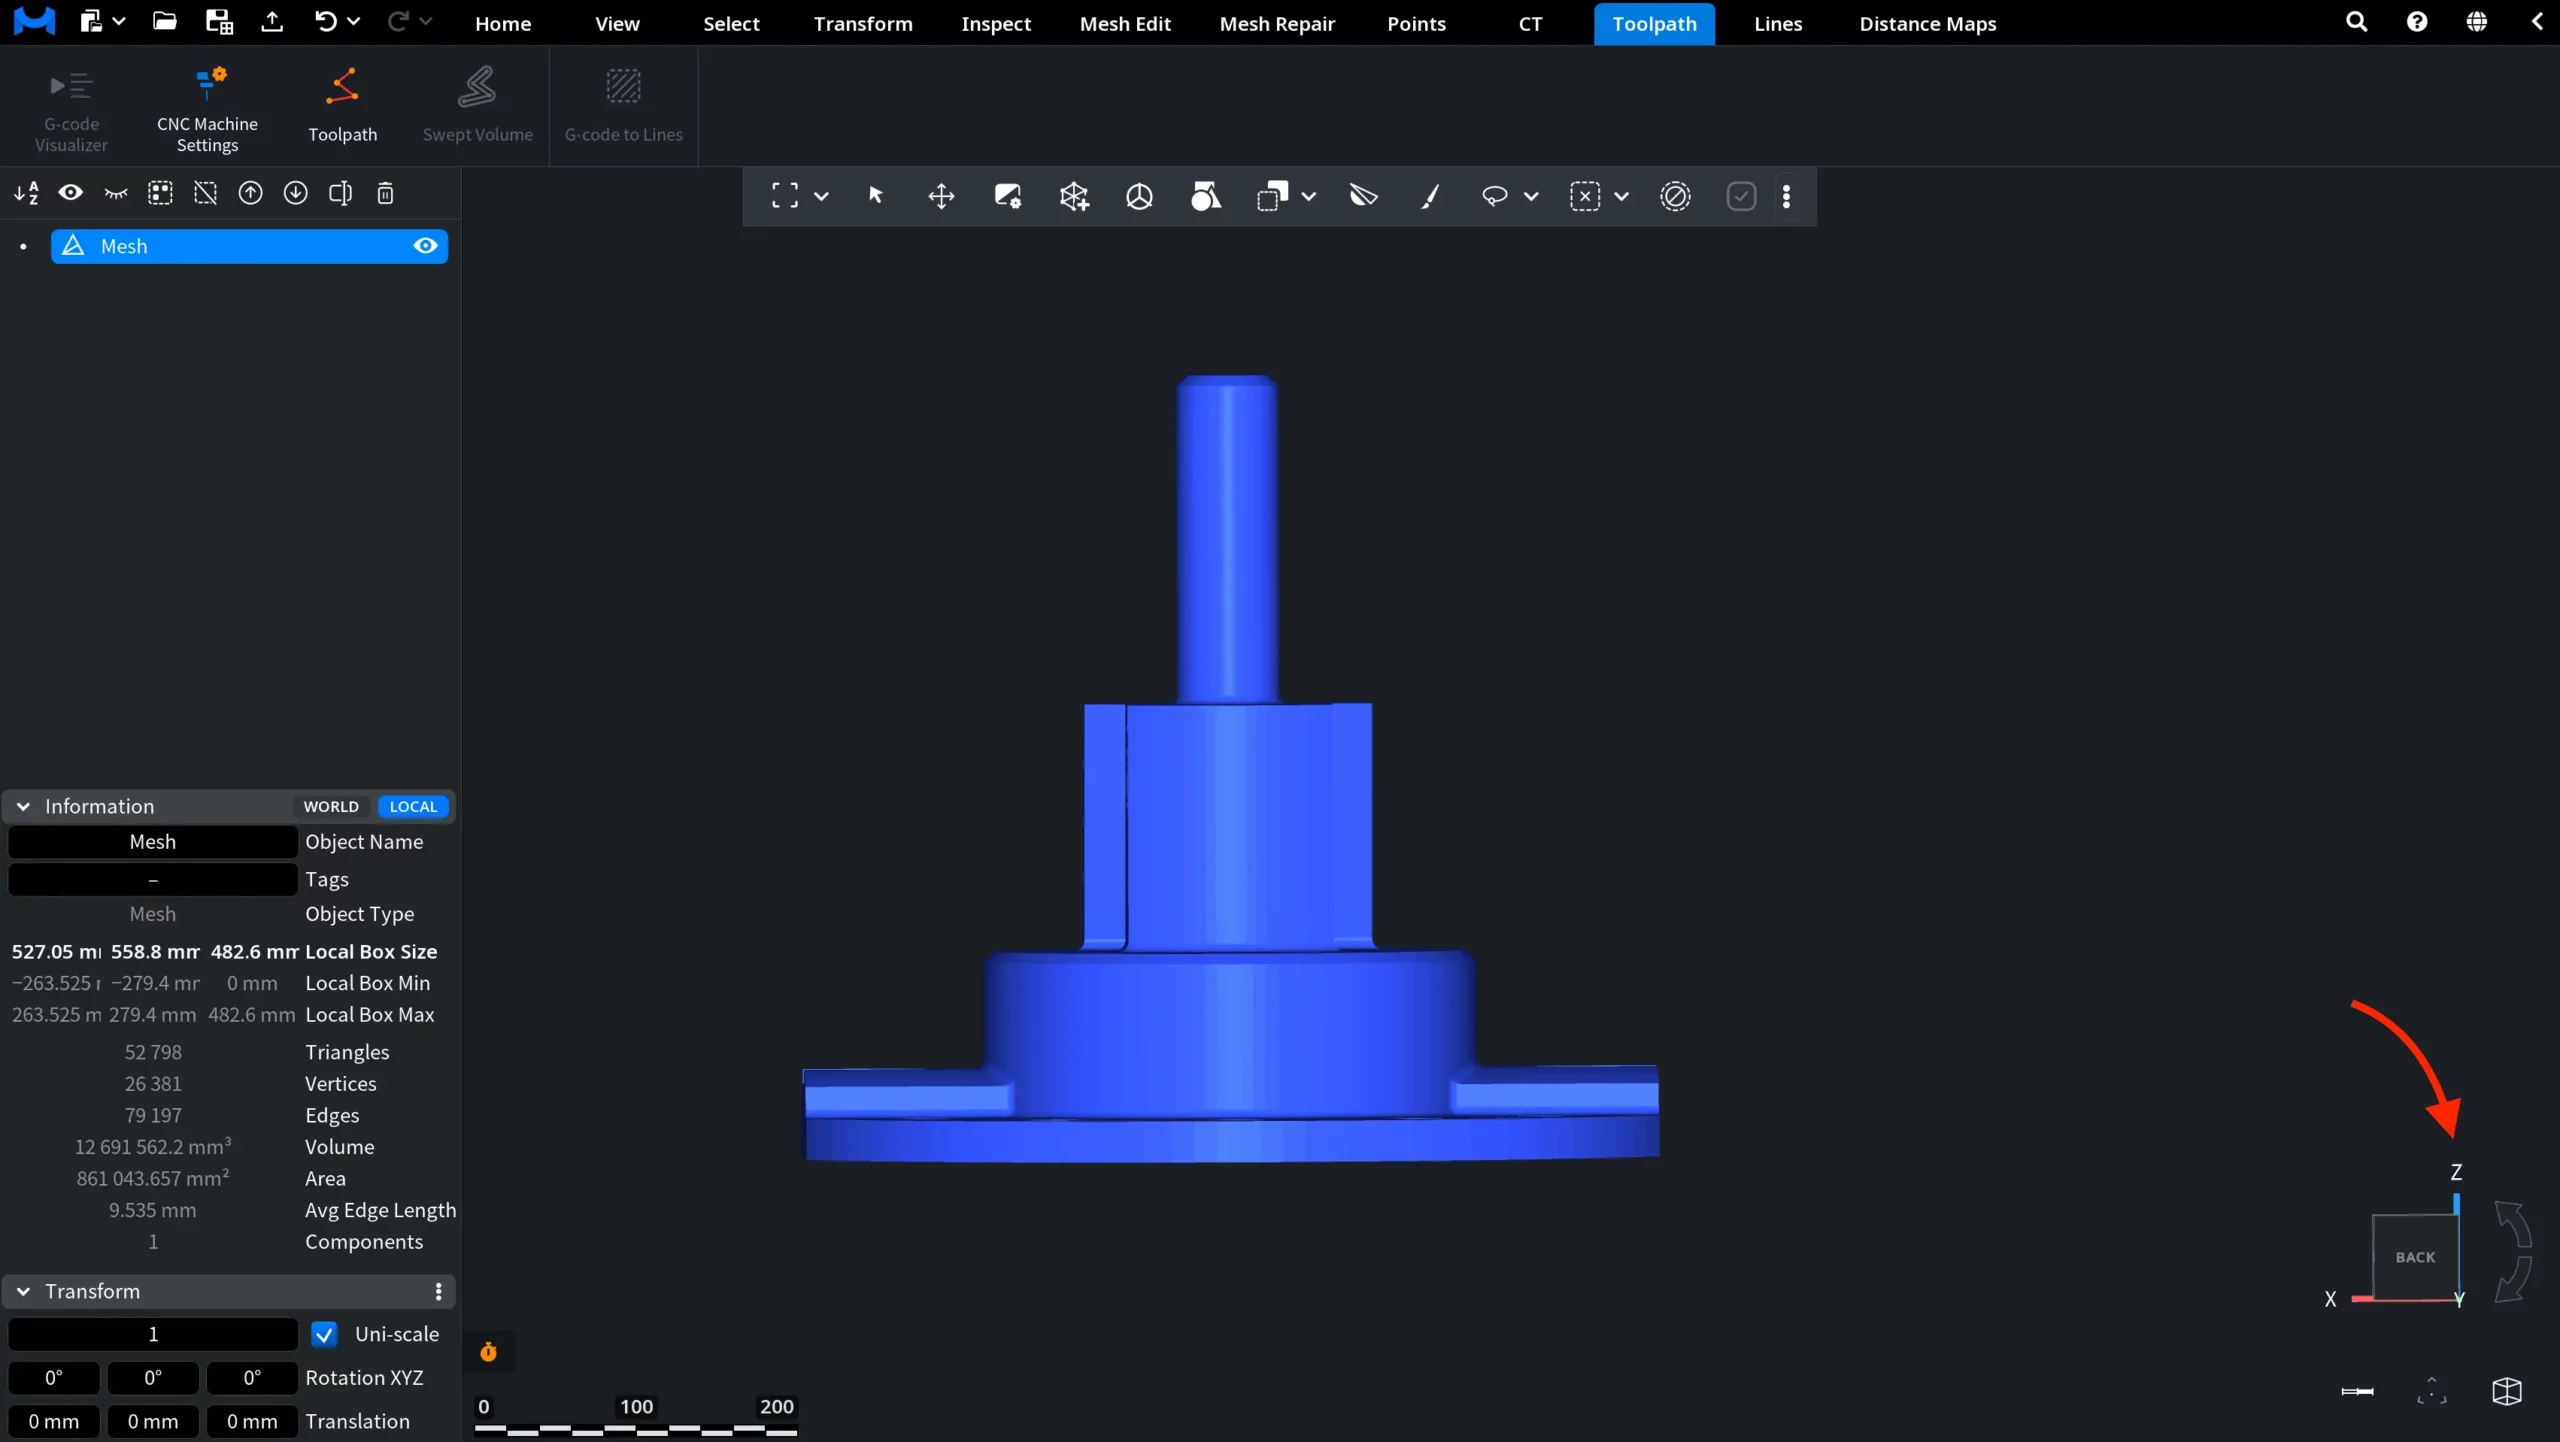
Build a toolpath
- Select exactly one mesh in the Scene tree. To mill only a part of the surface, select those faces first: the path is then built for the selected region only.
- Click Toolpath › Toolpath. The Toolpath panel opens; its values are calculated from the size of the part.
- Choose the Type of Tool Path and set the tool and the step over (see the tables below).
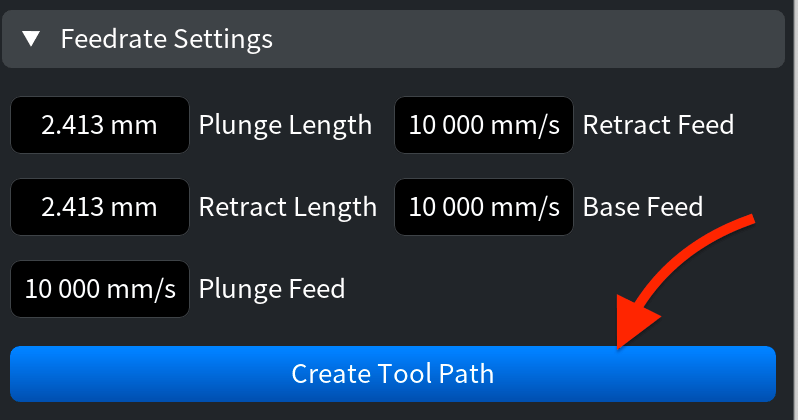
- Click Create Tool Path. The progress bar shows Tool Path: Constant Z (or the type you chose).
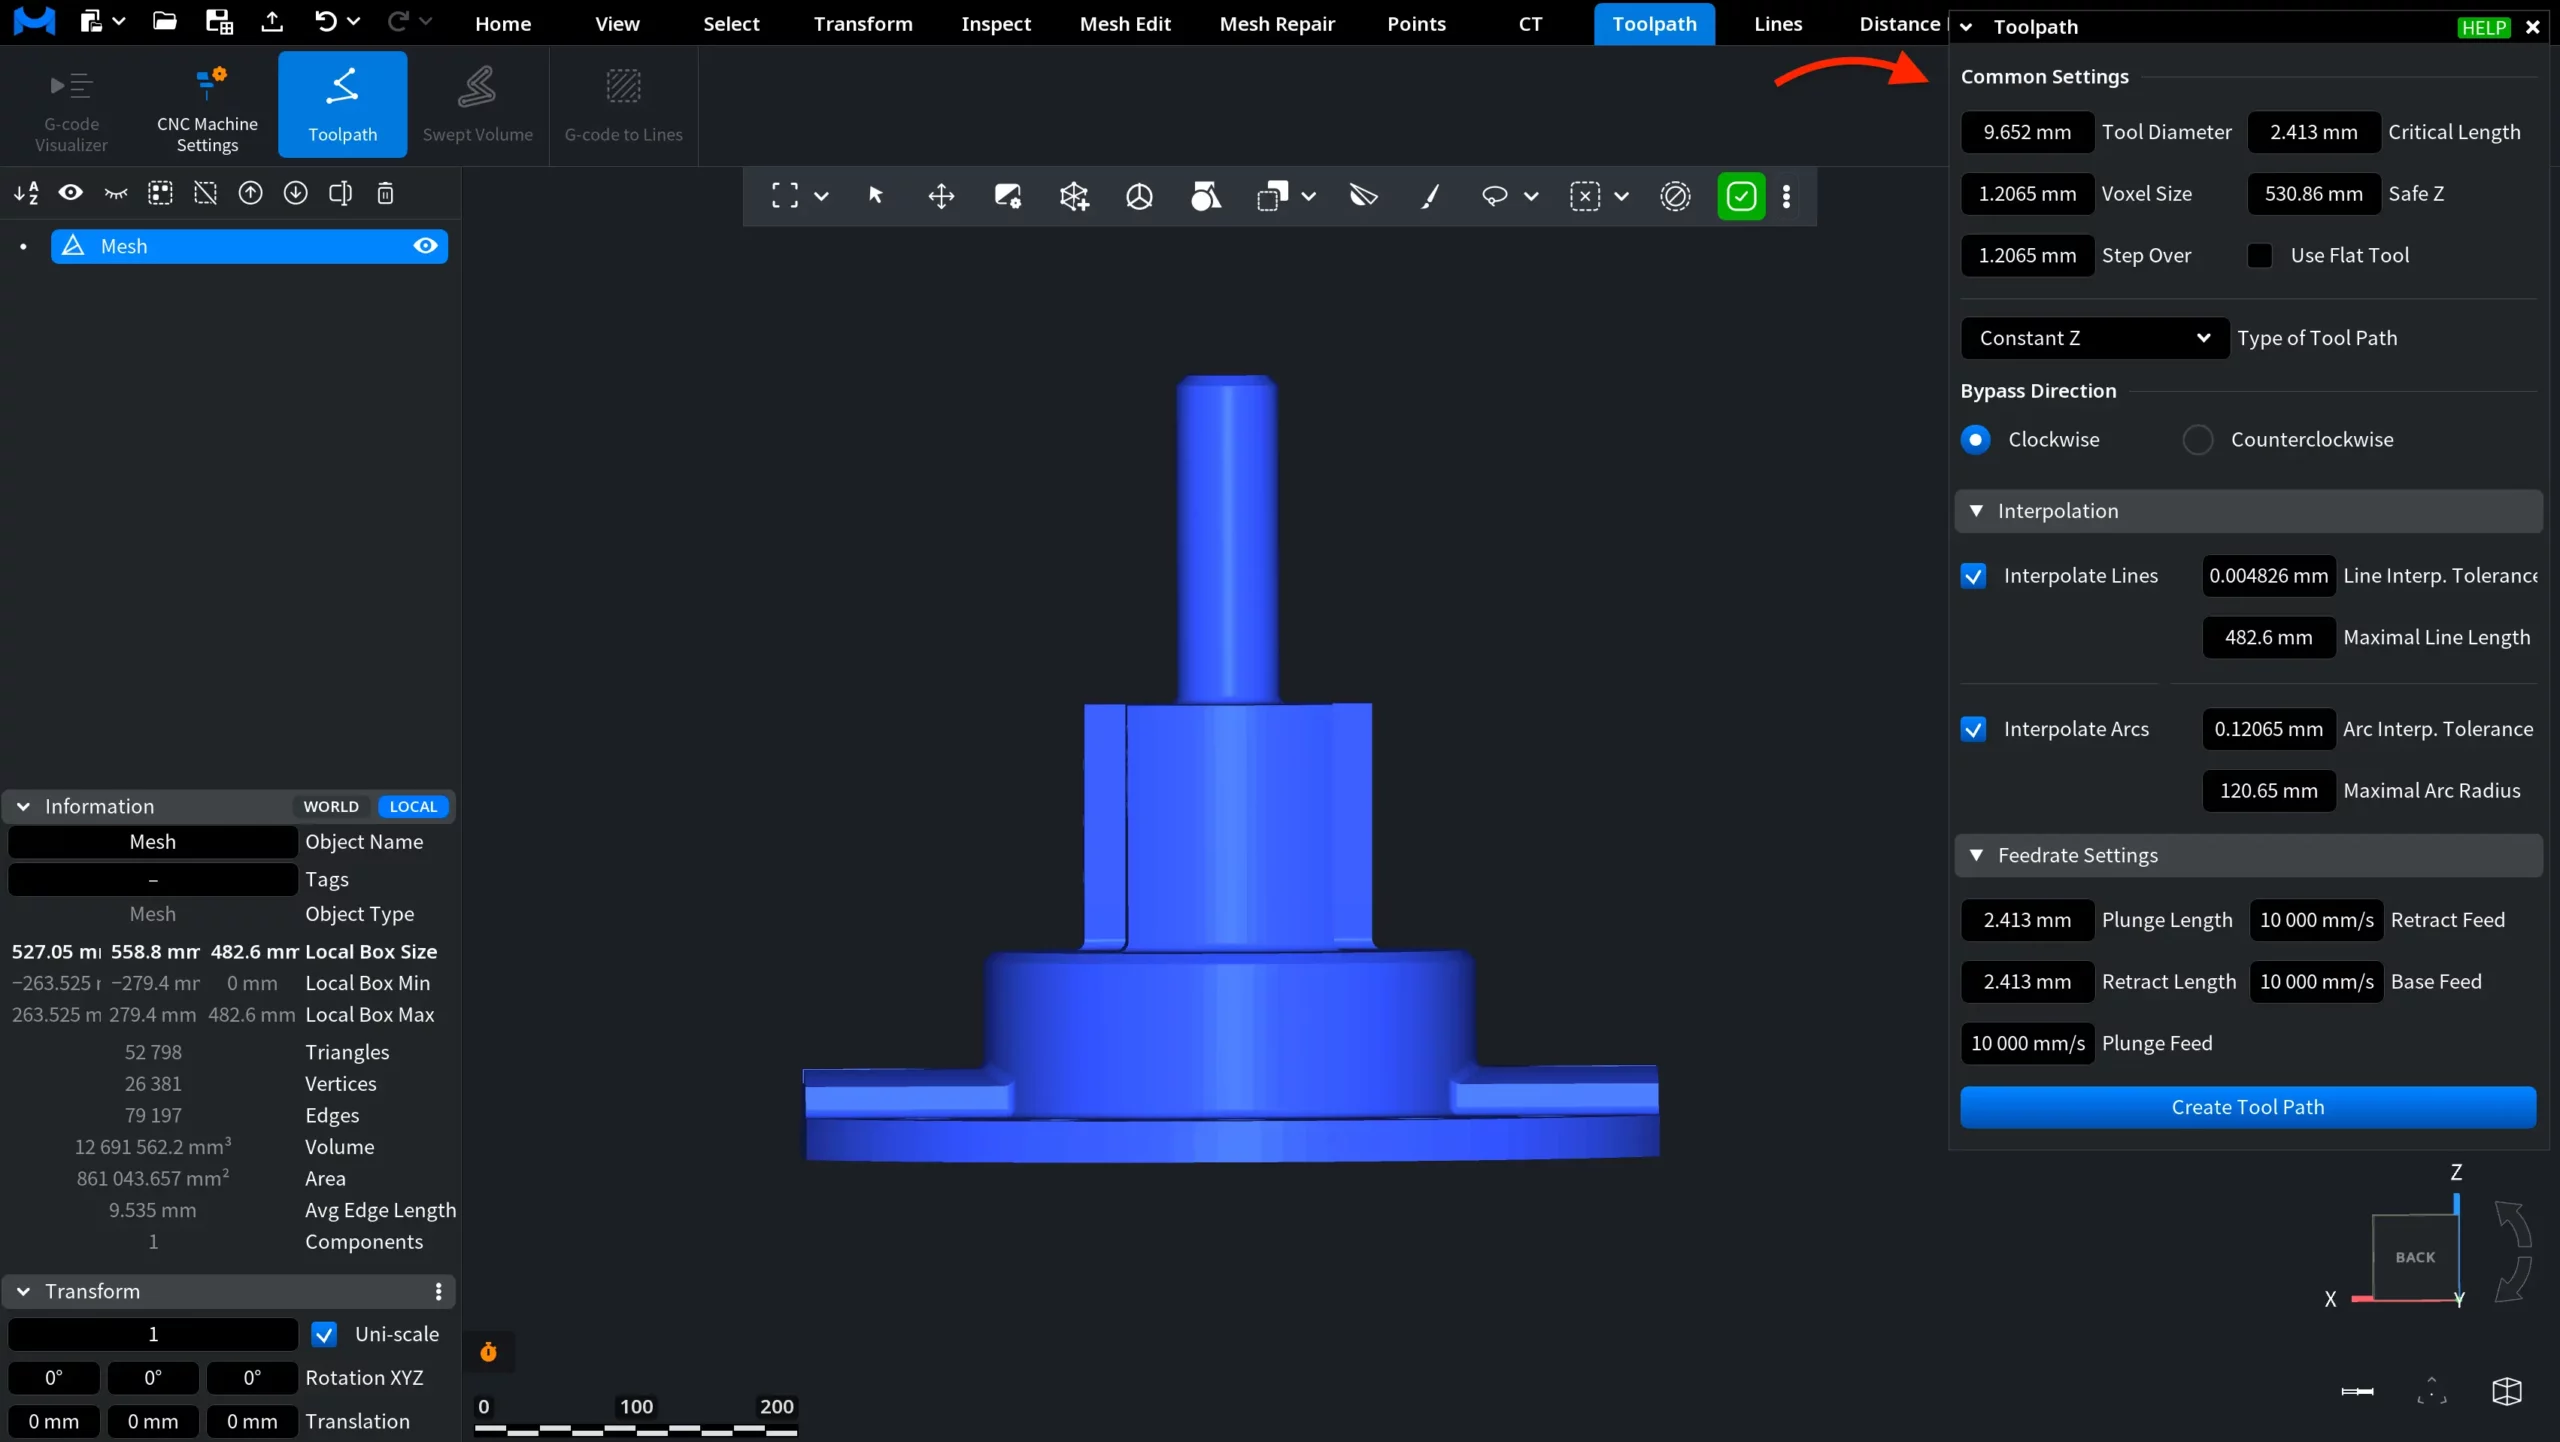
The result is a new G-code object named after the tool and the step, for example Tool Path_D0.2_ST0.025 (diameter 0.2, step over 0.025). Inside it is a mesh Tool_D0.2_ST0.025: a ball-end tool of the set diameter. The panel stays open, so you can change the type or the values and create another path for comparison.
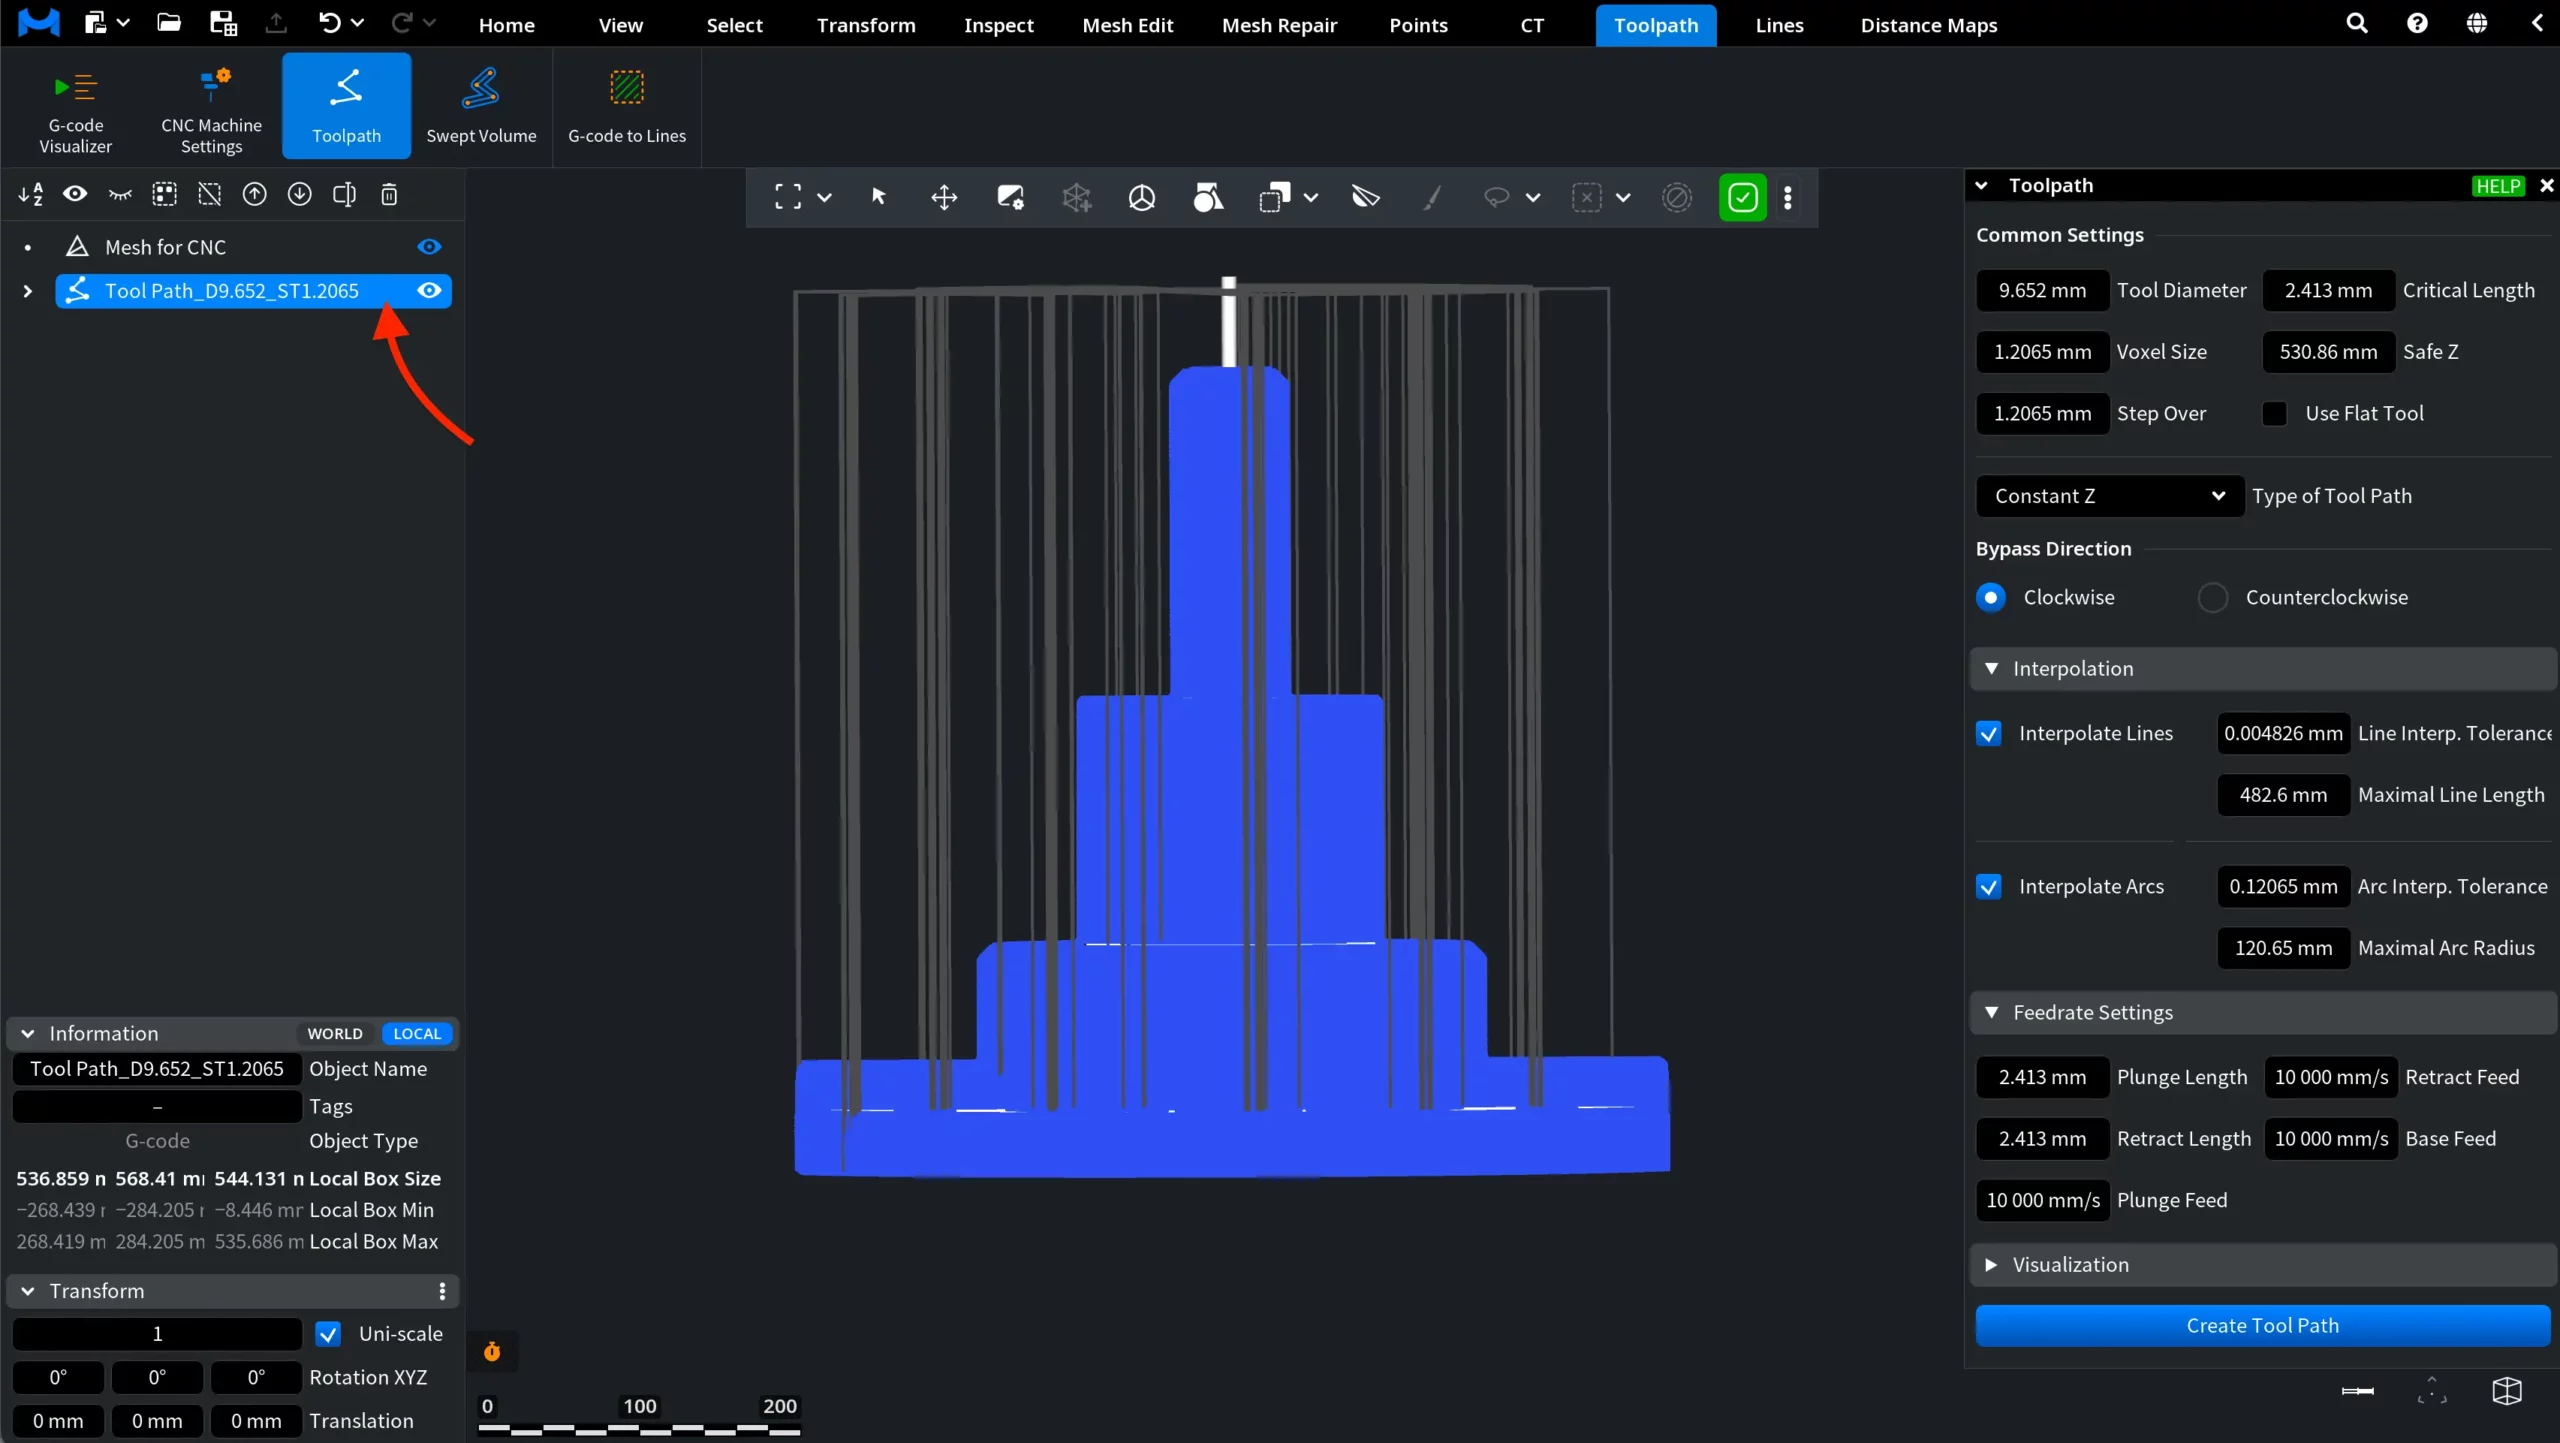
Types of toolpath
| Type | How the tool moves | Own settings |
|---|---|---|
| Constant Z | Cuts the part in horizontal layers, one Z level after another, and goes around the part in each layer | Bypass Direction, Use Flat Tool |
| Lacing | A raster (lace) path: the tool moves back and forth in parallel slices along X or Y and follows the surface | Lacing Direction, Toolpath in Empty Areas |
| Constant Cusp | Follows lines of equal distance along the surface that spread from a start point or from the boundary of the selected faces, Step Over apart | Bypass Direction, Mill From Center To Boundary |
- Bypass Direction (Constant Z and Constant Cusp): Clockwise (default) or Counterclockwise, the direction in which the sections or isolines are passed.
- Lacing Direction (Lacing): Axis X (default) or Axis Y.
- Toolpath in Empty Areas (Lacing, off by default): also builds passes around the part to mill away the excess material. Toolpath Expansion then sets how far this box-shaped area goes beyond the part.
- Mill From Center To Boundary (Constant Cusp, on by default): processes the isolines from the center point to the boundary, which usually means from top to bottom.
Common Settings
| Parameter | What it does | Default |
|---|---|---|
| Tool Diameter | Diameter of the milling tool | 2% of the part height, at least 0.2 |
| Voxel Size | Size of the voxels used to offset the mesh by the tool radius. Smaller is more exact and slower | ¼ of the tool radius; at most 0.3 of the radius |
| Step Over | Distance between neighboring sections (Constant Z: between Z levels) | ¼ of the tool radius; at most the radius. For Constant Cusp at least 1.2 × Voxel Size |
| Critical Length | If the next section is closer than this, the tool moves to it along the surface; otherwise it goes up through the safe plane | 2 × Step Over |
| Safe Z | Height of the plane where the tool can move in any direction without touching the part | Top of the part + 10 tool radii |
| Use Flat Tool | Builds the path for a flat end mill. Shown for Constant Z only; it is switched off when you change the type | Off |
For example, on a part 4.8 × 5.2 × 2.7 mm the panel opens with Tool Diameter 0.2 mm, Voxel Size and Step Over 0.025 mm, Critical Length 0.05 mm. When you switch the type to Constant Cusp, Step Over goes up to 0.03 mm (1.2 × Voxel Size).
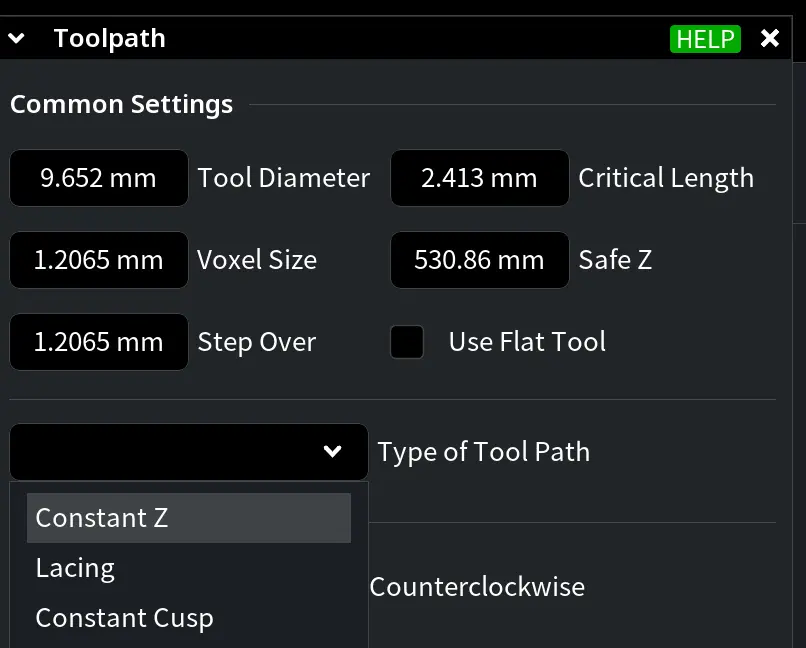
The tooltip of Tool Diameter says "Radius of the milling tool", but the field is the diameter: the tool mesh in the result has half of this value as its radius.
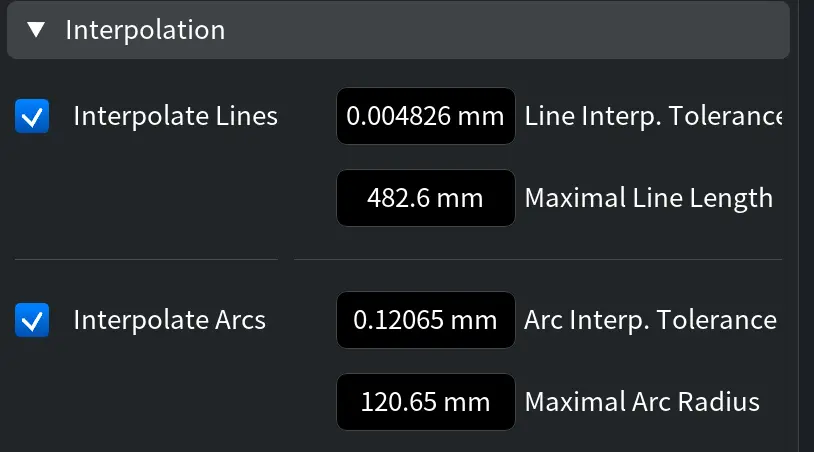
Interpolation
The collapsed Interpolation section replaces chains of short moves with longer lines and arcs, so the program gets shorter. It works for Constant Z and Lacing; a Constant Cusp path is not interpolated.
| Parameter | What it does | Default |
|---|---|---|
| Interpolate Lines | Joins moves into straight lines | On |
| Line Interp. Tolerance | Largest deviation of a line from the path | 0.001 × Step Over |
| Maximal Line Length | Longer segments are not optimized | Height of the part |
| Interpolate Arcs | Replaces suitable segments with arcs | On |
| Arc Interp. Tolerance | Largest deviation of an arc from the path | 0.1 × Step Over |
| Maximal Arc Radius | Arcs with a larger radius are not used | 1000 × Arc Interp. Tolerance |
Feedrate Settings
The collapsed Feedrate Settings section sets the feeds written into the program.
| Parameter | What it does |
|---|---|
| Plunge Length | Distance from the mesh at which the tool slows down when moving down (default 2 × Step Over) |
| Retract Length | Distance from the mesh at which the tool slows down when moving up (default 2 × Step Over) |
| Plunge Feed | Speed of the slow movement down |
| Retract Feed | Speed of the slow movement up |
| Base Feed | Speed of regular milling |
Use Flat Tool
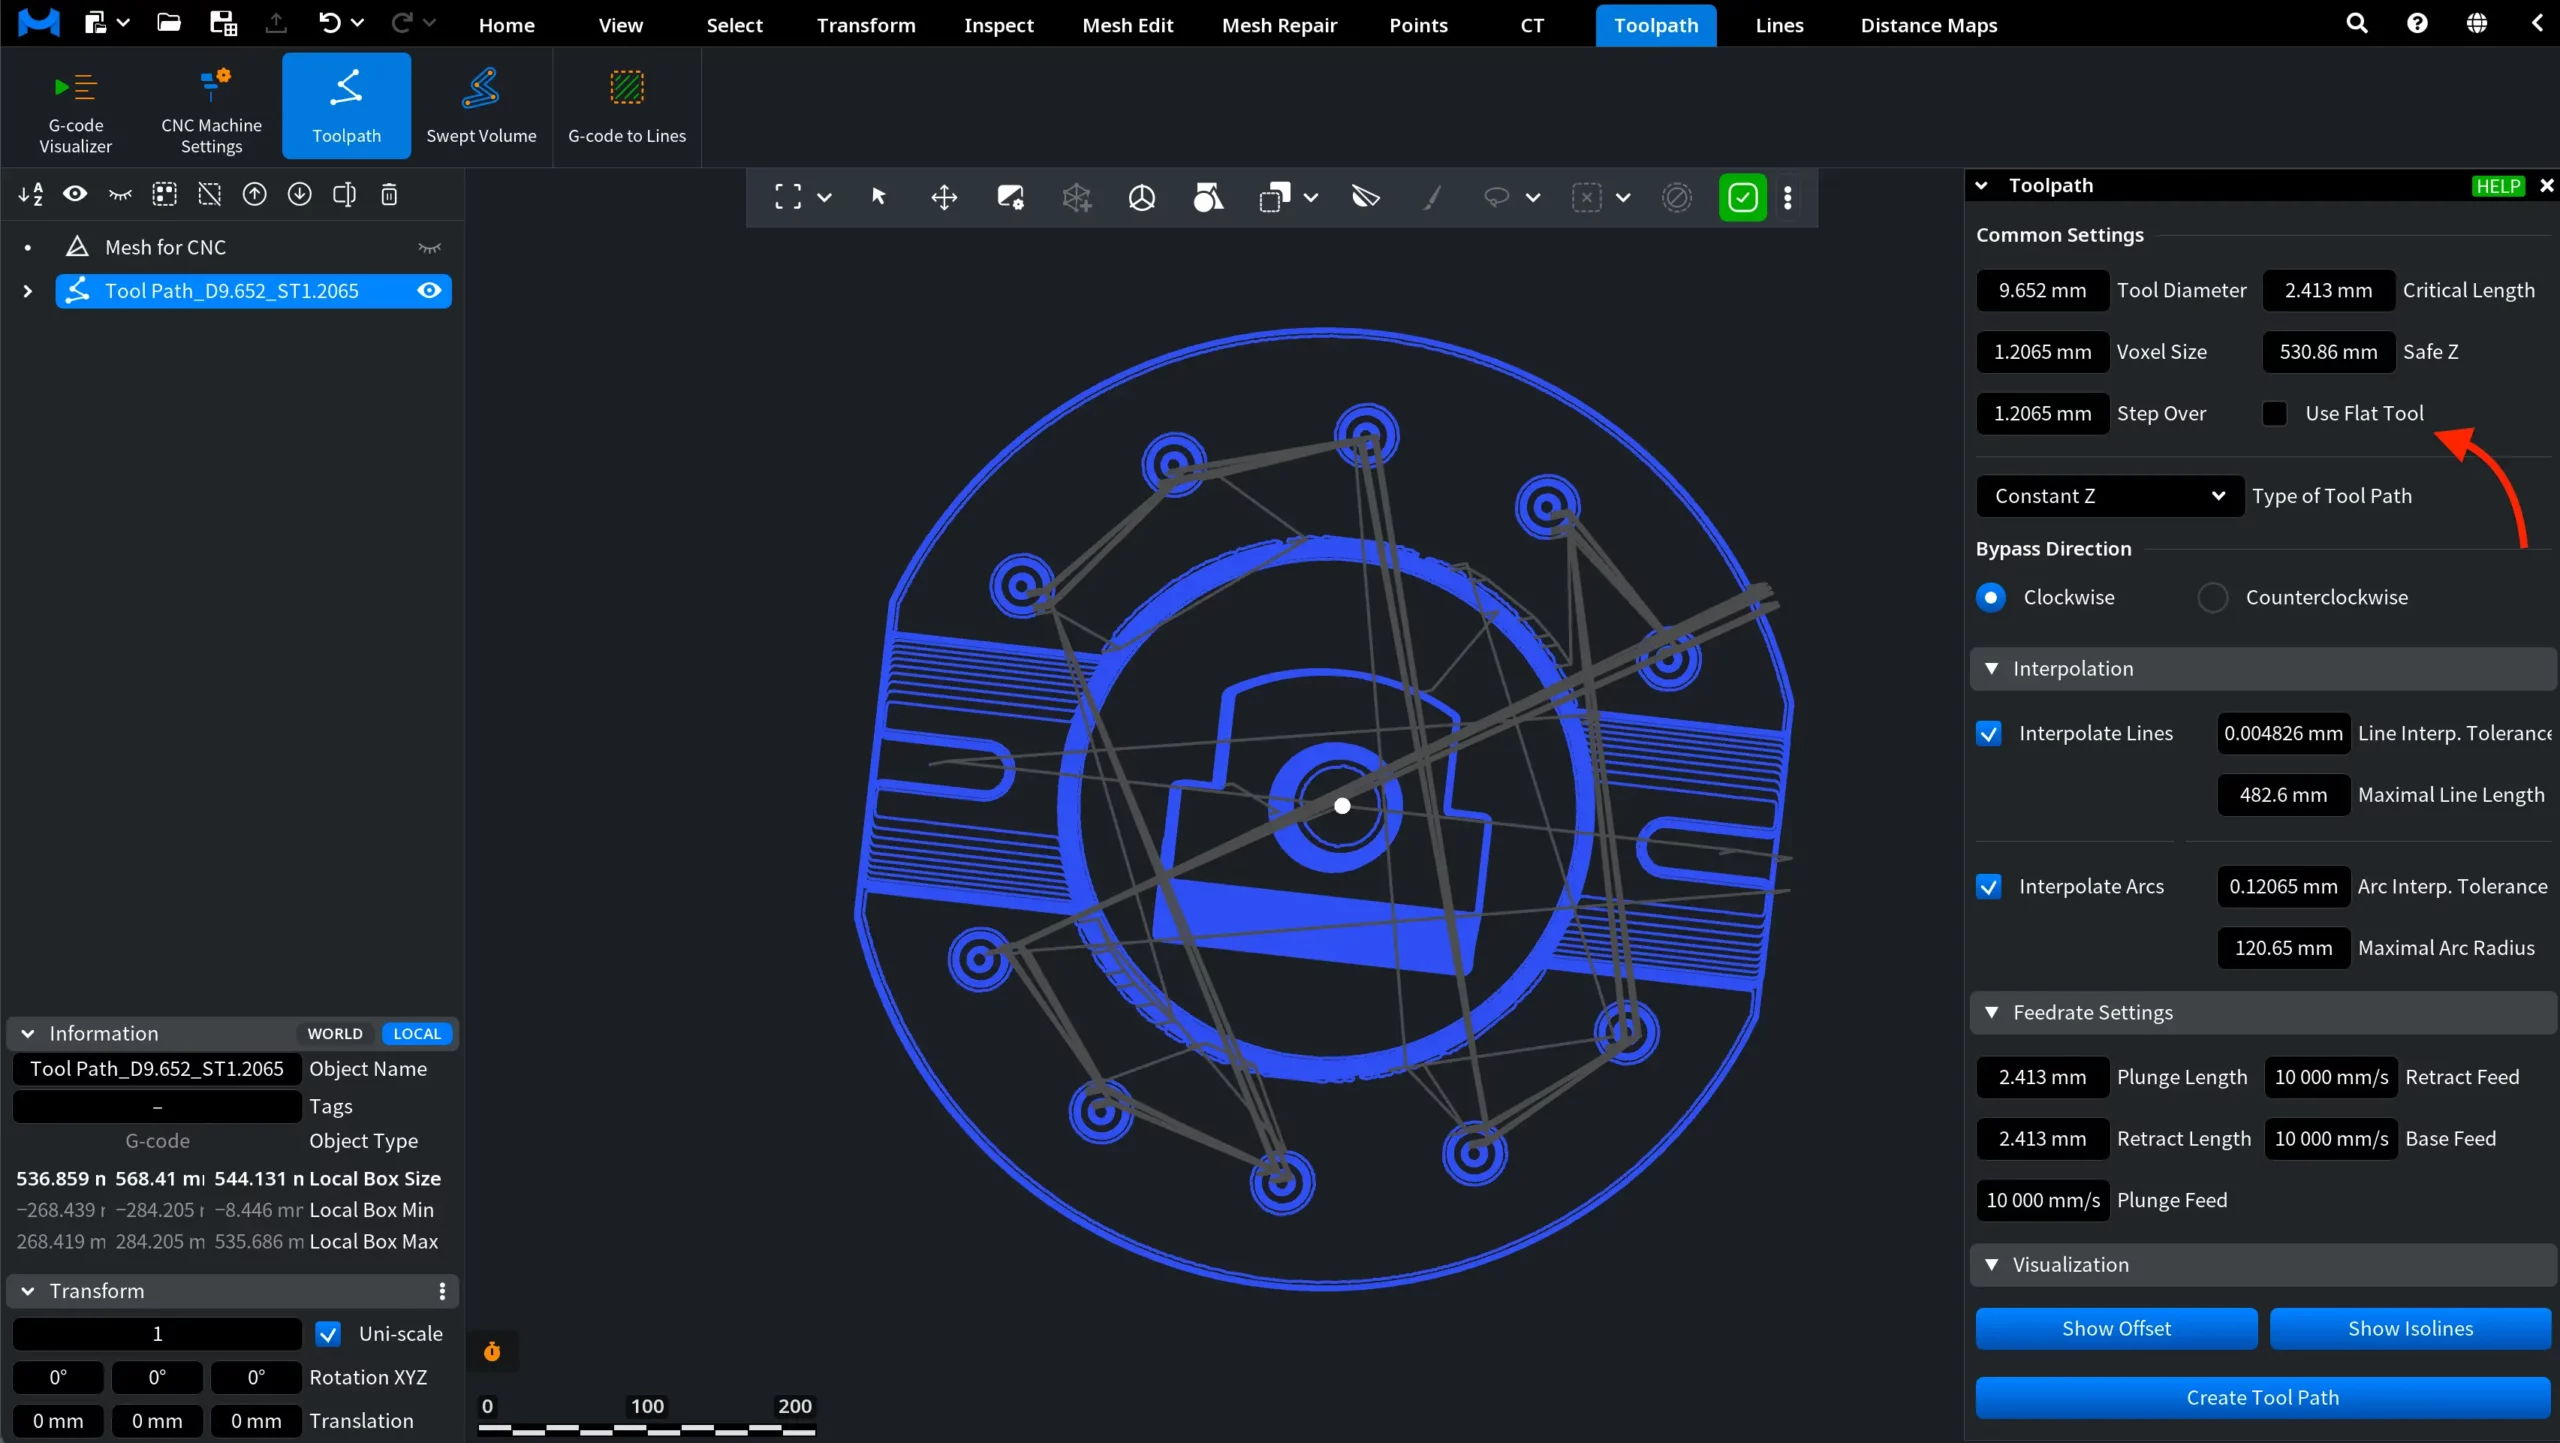
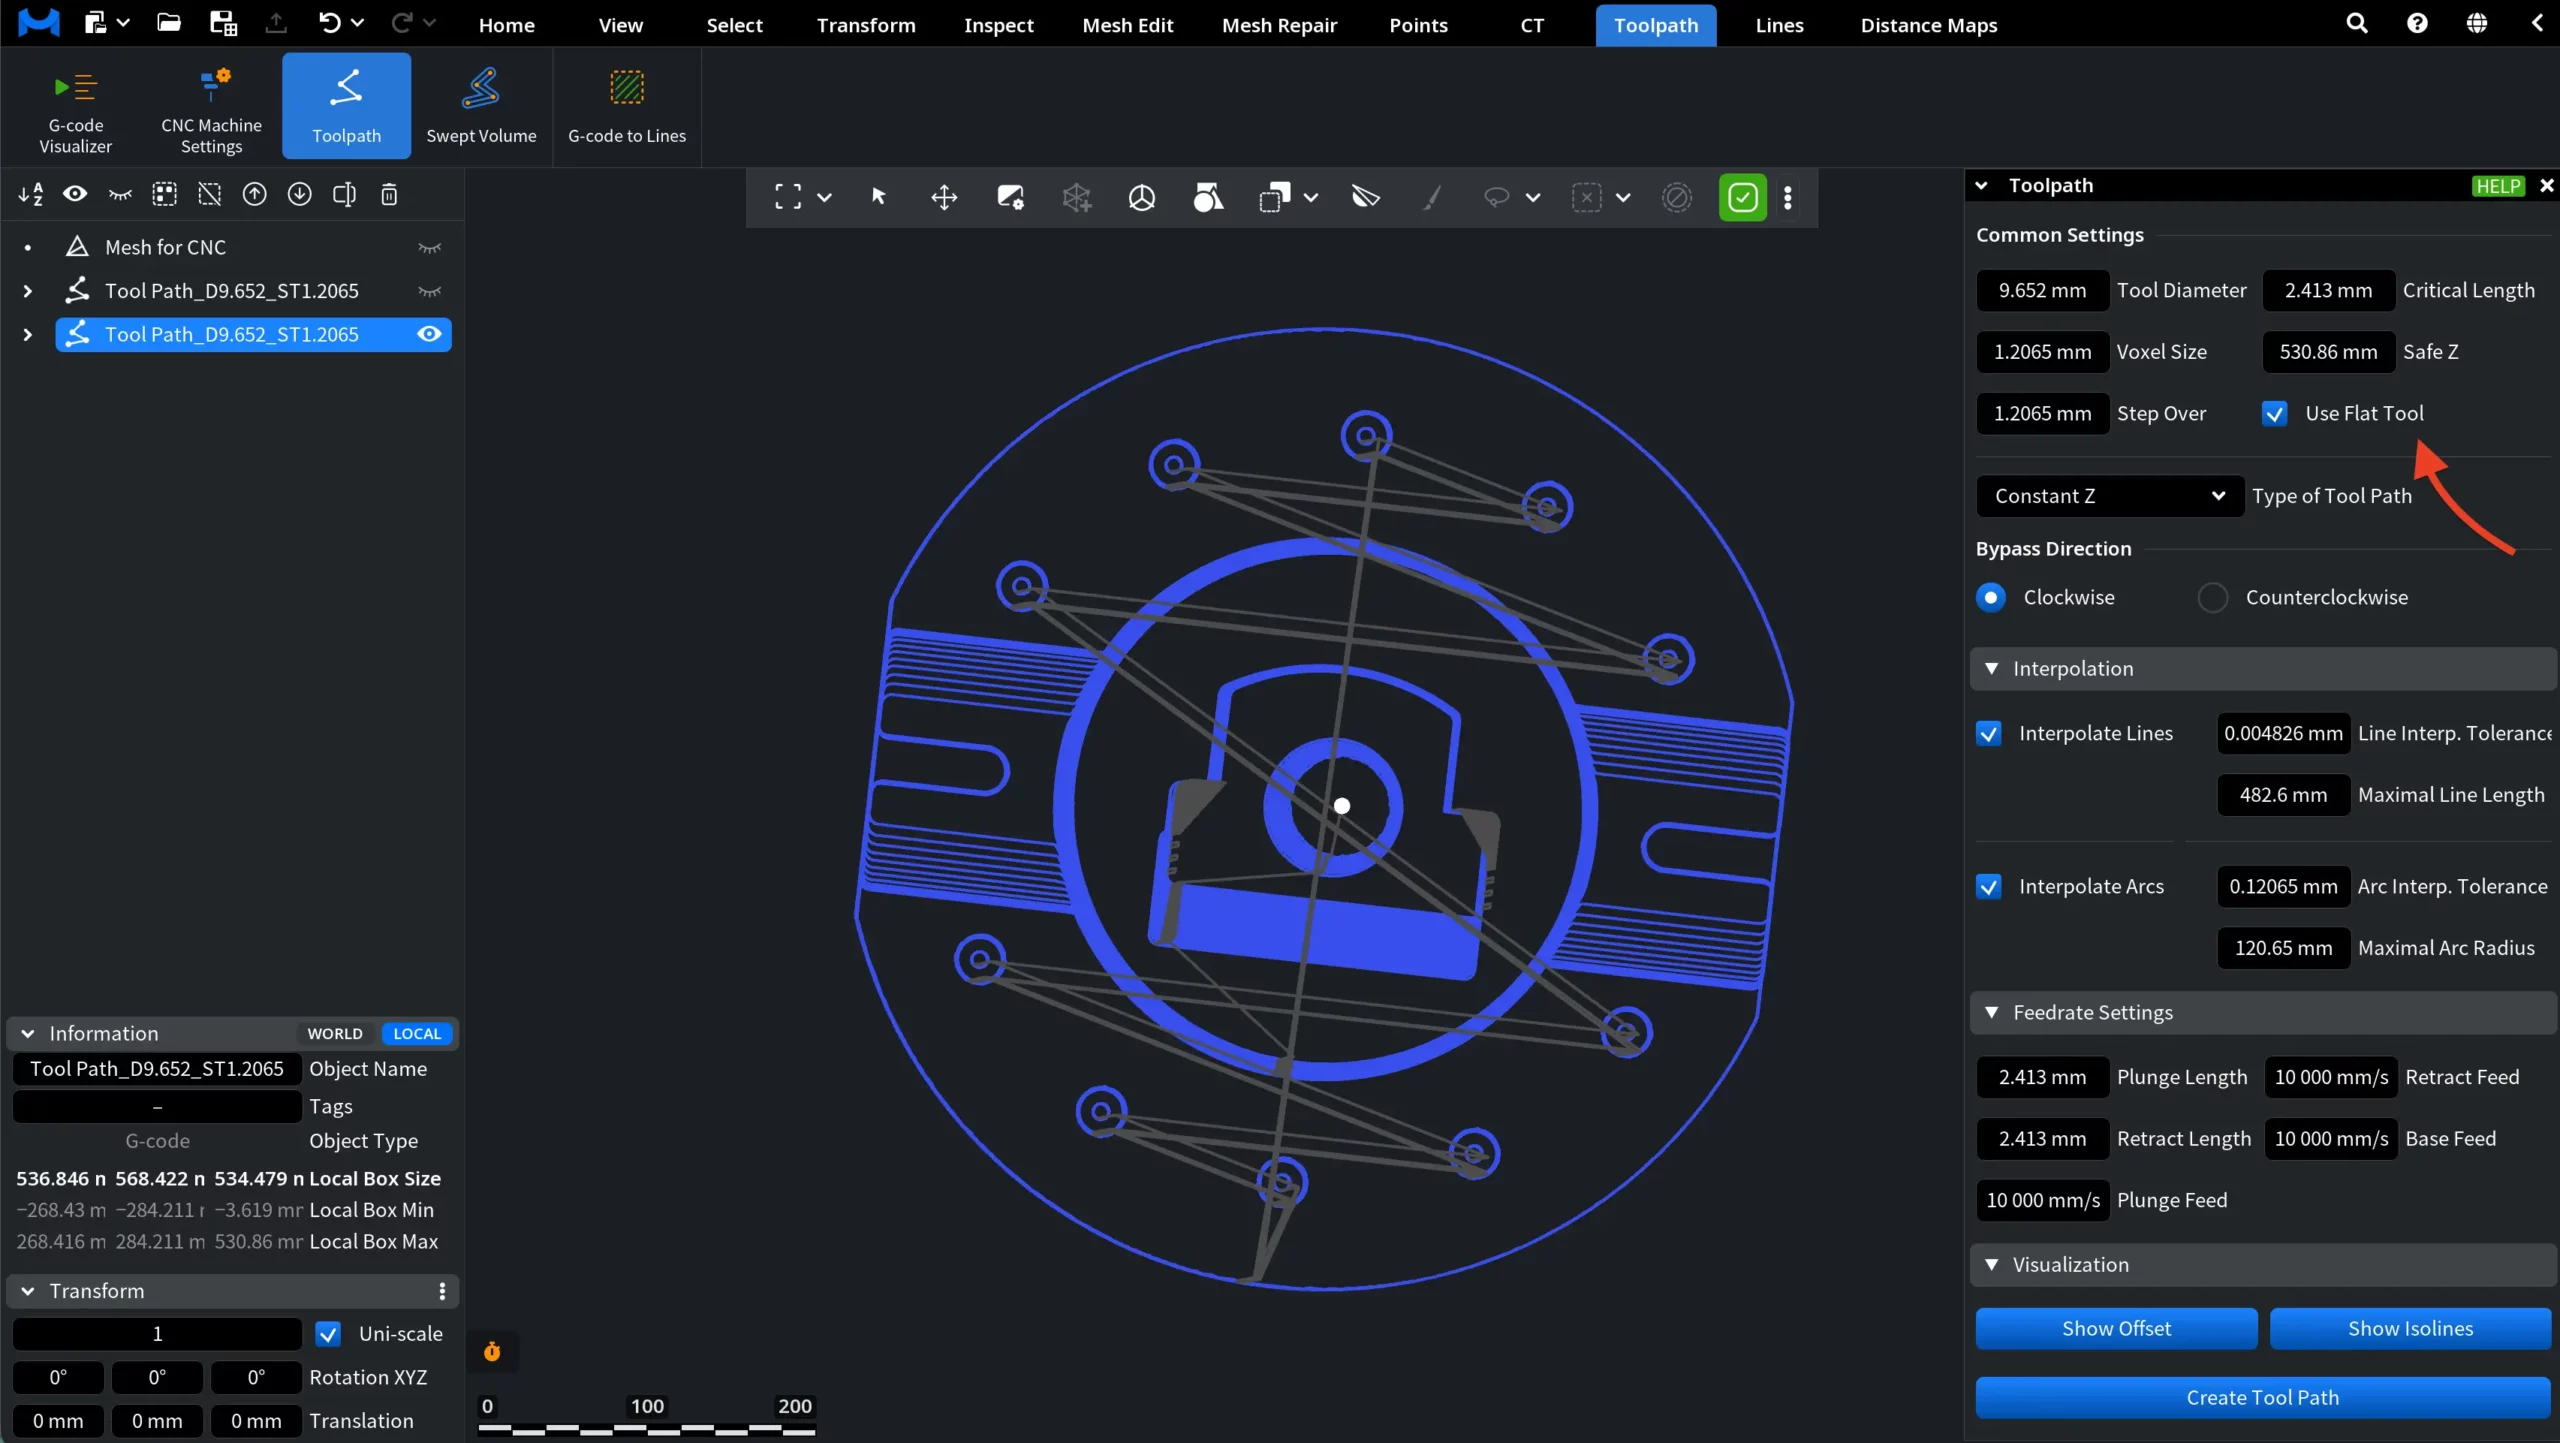
With Use Flat Tool off, the path is built for a ball-end tool. Turn it on for a flat end mill; this option exists for Constant Z only.

Here are both paths from above, with the part hidden: without and with Use Flat Tool.
Visualization
After the first path is created, the panel gets a collapsed Visualization section. Its buttons add helper objects under the part in the Scene tree:
- Show Offset: the offset mesh the path is built on (the part after undercuts are filled and the surface is offset), named after the part with Offset added.
- Show Isolines: the sections or isolines used to build the path, named after the part with Isolines added.
- Show Start Contours and Show Start Vertices: where the passes start, as green lines and as points. They appear only when the last path has such data.
Check and keep the result
- Select the Tool Path… object and open Toolpath › G-code Visualizer to read the program line by line and play the tool along it.
- Toolpath › Swept Volume builds the space the tool occupies along the path, to compare it with the part.
- MeshInspector does not write G-code files: with a G-code object selected, Export is unavailable ("Select objects of the same type (e.g. Meshes, Point Clouds or Volumes)"). Save Scene keeps the path in a scene file (.mru); G-code to Lines turns it into a polyline that you can export.

